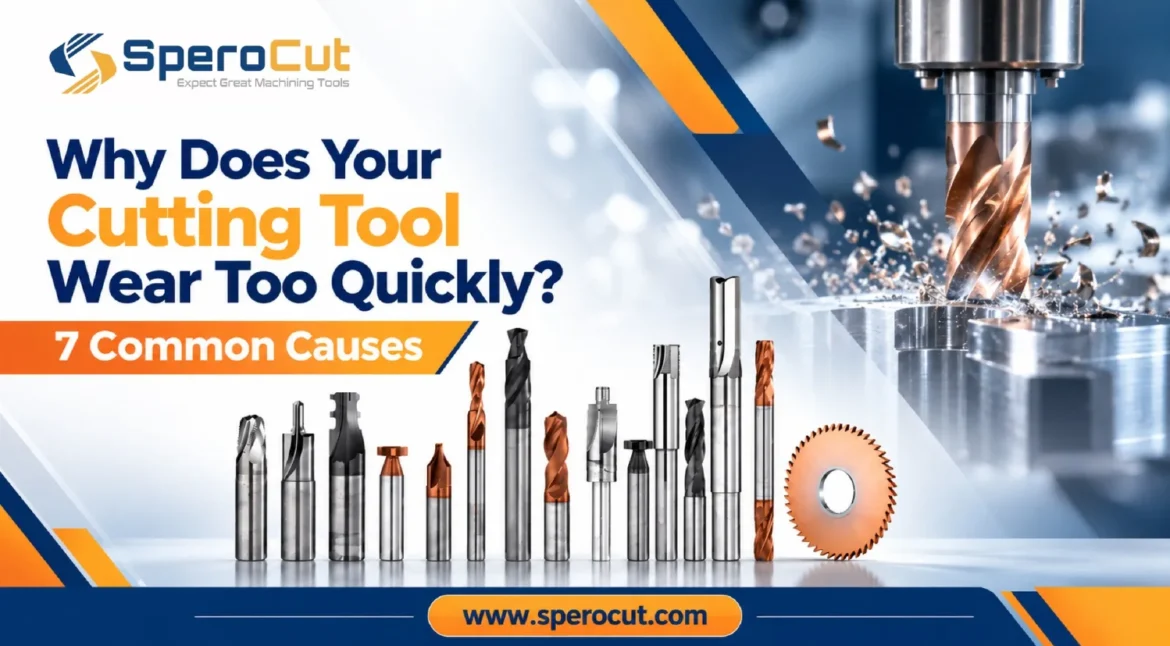
Cutting tool wear is one of the most common challenges in CNC machining. When a tool wears faster than expected, it can lead to poor surface finish, dimensional inaccuracies, increased cycle time, tool breakage, and higher production costs.
For manufacturers working with demanding materials such as steel, stainless steel, cast iron, titanium, and other hard materials, choosing the right cutting tool and machining parameters is essential for achieving consistent performance.
SperoCut Tools manufactures high-precision carbide cutting tools for applications across automotive, aerospace, medical, defense, forging, and general engineering industries. Its product range includes drills, end mills, reamers, hole mills, ball nose end mills, cutters, micro drills, special tools, and customized tooling solutions.
But even a high-quality cutting tool can experience premature wear if the machining process is not optimized.
So, why does your cutting tool wear too quickly? Here are seven common causes.
1. Incorrect Cutting Speed
One of the most common causes of premature cutting tool wear is incorrect cutting speed.
If the cutting speed is too high, excessive heat can develop at the cutting edge. This can accelerate flank wear, crater wear, edge chipping, and even tool failure.
On the other hand, cutting too slowly can also create problems depending on the application, material, tool geometry, and machining conditions.
The correct cutting speed depends on factors such as:
- Workpiece material
- Tool material
- Tool diameter
- Tool coating
- Machine capability
- Cutting operation
- Depth of cut
- Feed rate
Tip: Always select cutting parameters based on the specific tool, material, and machining application rather than relying on a general setting.
2. Incorrect Feed Rate
Feed rate has a direct impact on cutting forces and tool life.
A feed rate that is too high can overload the cutting edge, resulting in excessive mechanical stress, vibration, chipping, or breakage.
A feed rate that is too low can also be problematic. In some applications, the tool may rub against the workpiece instead of cutting efficiently, generating unnecessary heat and accelerating wear.
The ideal feed rate should provide an effective balance between productivity, cutting force, surface finish, and tool life.
For precision machining, feed per tooth and chip load should be considered rather than simply increasing or decreasing feed based on production requirements.
3. Choosing the Wrong Cutting Tool
Not every cutting tool is suitable for every machining application.
Using the wrong tool geometry, diameter, flute configuration, coating, or substrate can significantly reduce tool life.
For example, machining hardened steel requires different tooling considerations compared with aluminium or non-ferrous materials. Similarly, deep-hole drilling, high-speed milling, slotting, and finishing operations require different tool designs.
SperoCut manufactures specialized carbide tools for different applications and materials, including steel, titanium, cast iron, non-ferrous metals, and hard materials. The company also develops special tools according to customer requirements.
The right tool is not simply the strongest tool—it is the tool designed for the specific machining application.
4. Poor Tool Holding and Runout
Even a premium cutting tool can perform poorly if it is not held correctly.
Excessive tool runout means the cutting edges are not sharing the machining load evenly. One flute may remove more material than the others, resulting in:
- Uneven tool wear
- Poor surface finish
- Increased vibration
- Dimensional variation
- Reduced tool life
- Premature edge failure
Proper tool holding, machine spindle condition, collet quality, tool concentricity, and correct tightening are therefore critical.
For high-precision machining, maintaining proper tool alignment can make a significant difference in tool performance.
5. Inadequate Coolant or Lubrication
Heat is a major factor in cutting tool wear.
During machining, friction between the cutting tool and workpiece generates heat. If that heat is not effectively controlled, the cutting edge can deteriorate faster.
Insufficient coolant flow, incorrect coolant concentration, poor coolant delivery, or ineffective chip evacuation can all contribute to excessive cutting temperatures.
For some applications, coolant-through tooling can improve coolant delivery directly to the cutting zone. SperoCut, for example, offers solid carbide tooling configurations that include coolant-through options for certain applications.
However, coolant requirements vary depending on the material, tool, machine, and machining operation.
6. Poor Chip Evacuation
Efficient chip evacuation is particularly important during drilling, deep-hole machining, slotting, and other operations where chips can accumulate around the cutting zone.
When chips are not removed effectively, they can:
- Re-enter the cutting zone
- Increase friction
- Generate excessive heat
- Damage the cutting edge
- Scratch the machined surface
- Cause tool breakage
Tool geometry plays an important role in chip control.
For example, SperoCut’s carbide drill designs incorporate specialized flute geometry intended to support chip evacuation and reduce cutting resistance.
Selecting the appropriate flute design, coolant method, feed rate, and cutting parameters can significantly improve chip evacuation.
7. Machine Vibration and Lack of Rigidity
Vibration, commonly known as chatter, is another major contributor to premature cutting tool wear.
Chatter can occur because of:
- Insufficient machine rigidity
- Poor workpiece clamping
- Excessive tool overhang
- Incorrect cutting parameters
- Worn machine components
- Improper tool geometry
Continuous vibration puts additional stress on the cutting edge and can result in chipping, uneven wear, poor surface finish, and reduced tool life.
Reducing tool overhang, improving workholding, optimizing cutting parameters, and selecting an appropriate tool geometry can help create a more stable machining process.
How Can You Increase Cutting Tool Life?
Extending cutting tool life is not only about buying a better tool. It requires a combination of correct tool selection, optimized machining parameters, proper setup, and regular inspection.
Consider the following practices:
Select the Right Tool
Match tool geometry, coating, diameter, and substrate to the material and application.
Optimize Cutting Parameters
Use appropriate cutting speed, feed rate, depth of cut, and chip load.
Maintain Proper Tool Holding
Minimize runout and unnecessary tool overhang.
Control Heat
Use an appropriate coolant or lubrication strategy where required.
Improve Chip Evacuation
Ensure chips are removed efficiently from the cutting zone.
Monitor Tool Wear
Inspect tools regularly instead of waiting for complete failure.
Consider Regrinding & Recoating
Where suitable, tool reconditioning can help extend the usable life of cutting tools. SperoCut provides regrinding and recoating facilities for different types of tools.
The Right Tool Can Make a Difference
Premature cutting tool wear is rarely caused by just one factor. Tool selection, machining parameters, workholding, coolant, chip evacuation, and machine stability all influence cutting performance.
A properly selected and optimized cutting tool can help manufacturers achieve better tool life, improved surface finish, greater dimensional consistency, and reduced machining costs.
SperoCut focuses on precision carbide cutting tools and customized tooling solutions designed around specific machining requirements. Its manufacturing and inspection capabilities include advanced CNC tool grinding and precision measurement systems to maintain tool geometry, accuracy, and consistency.
Great machining results start with the right tool.
If you are experiencing premature tool wear or looking for a cutting tool optimized for a specific machining application, the right technical consultation can help identify the underlying problem and improve overall tool performance.